Hey everyone, if you’re in the rubber product manufacturing game, you’ve probably spent way too much time troubleshooting drying processes—whether it’s leftover moisture in cured gaskets, unevenly dried rubber seals that warp right when you need them, or that weird wait time after washing molded parts before you can move to the next step. Today I’m dropping a real, no-BS answer to a question I get every single week as a drying oven supplier: Can a drying oven actually be used for drying rubber products? Spoiler alert: It’s not a one-size-fits-all yes or no, and getting it right can save you from tons of scrap and headaches. Drying Oven

First, let’s ground this in what we’re actually dealing with when we talk about rubber drying. A lot of folks mix up two big types of moisture in rubber: surface moisture and bound moisture. If you just demolded a rubber part right out of a water-based cure (like common with silicone or nitrile for food-grade stuff) or pressure washed a batch of rubber hoses to remove release agent, that’s surface moisture—like a thin layer of water on the outside. But if you’re dealing with cured rubber that’s been sitting in a humid warehouse, or raw rubber compound that has residual moisture from mixing, that’s bound moisture trapped in the polymer chains or filler materials (like carbon black or silica). That’s the stuff that causes real issues: bubbles forming in your final product when you vulcanize it, reduced tensile strength, or even failure in extreme conditions.
Now, here’s the core question: Does a standard drying oven work for this? The short answer is, if you use the wrong oven or wrong settings, you’re gonna ruin parts. I’ve seen guys crank a $500 batch of rubber seals at 200°F in a cheap countertop oven, pull them out, and find they’re sticky, cracked, or have tiny blisters all over. Why? Rubber is a heat-sensitive material. Most standard rubber products (think nitrile, EPDM, silicone, natural rubber) have a cure temperature range, and if you hit them too fast or too hot, you get what’s called “pre-curing” or scorching. That’s when the rubber starts cross-linking before it’s supposed to, making it rigid, brittle, or unusable.
But wait—when you use a drying oven designed for rubber processing, it’s totally different. Let’s break down the right way to do this, because that’s what my team and I teach every customer who comes to us confused about their rubber drying. First, temperature control is non-negotiable. For surface moisture on molded rubber parts, you want to keep temps between 120°F and 170°F. That’s hot enough to evaporate water fast, but not hot enough to start any vulcanization or damage the polymer. For bound moisture in raw rubber compound or cured parts that sat around, you can bump it up a little—maybe 175°F to 190°F—but only if your oven has precise, uniform temperature. A lot of cheap drying ovens have hot spots, so one shelf is 190°F and another is 210°F, and that’s where scorch happens.
Next, air flow. This is another big one I see new guys mess up. Drying is all about moving humid air away from the part, right? If your oven has weak, unbalanced air flow, the air around the rubber gets saturated with water vapor, and evaporation grinds to a halt. For rubber, especially parts with small crevices or intricate shapes (like O-rings or gaskets), you need convection drying. That’s when the oven has fans that circulate air evenly around every inch of the load. I always tell customers: If you can hold a piece of thin paper up to the exhaust vent of your oven and it doesn’t flutter, your air flow is too weak, and you’re wasting time and energy.
Wait, what about specific rubber types? Because silicone is way different from natural rubber, right? Silicone is actually a bit more heat-tolerant, so you can dry it at 150°F to 180°F without scorch, which makes sense because it’s often used for high-heat applications. But EPDM, which is common for weather stripping, is more prone to discoloring if you run it too hot—so stick to the lower end of the range. Nitrile, used for hoses and seals, falls right in the middle. And don’t even get me started on rubber mixed with fillers like silica—those hold way more bound moisture, so you have to slow the process down. Trying to rush silica-filled rubber drying is how you get those tiny bubbles that make your parts fail a pressure test.
Now, let’s talk about common mistakes that make people think drying ovens don’t work for rubber. First, using a general-purpose oven that’s not made for heat-sensitive materials. I had a customer last month who was using a lab oven he already had in his R&D space to dry raw rubber compound. That oven was designed for drying solvents and metals, so it heated up way too fast, and his compound scorched before the moisture could even evaporate. We swapped him to a conveyor drying oven with a ramp-up temperature feature—so it heats the compound gradually over the first 10 minutes, then holds it steady at 180°F—and now he’s getting 0 scrap from moisture issues. Second, overloading the oven. If you stuff every shelf so tight that air can’t circulate between parts, you’re just drying the outside of the load, and the inside stays moist. Third, not accounting for part size. A small O-ring dries in 30 minutes, but a big rubber hose that’s 2 feet long needs an hour and a half minimum. I always tell people to test a small batch first—run a pilot load with 5-10 parts, track the weight before and after, and adjust time and temp until they hit the consistent dry weight they need.
Wait, is there a case where you shouldn’t use a drying oven for rubber? Let’s be real—if you’re dealing with super delicate rubber products, like thin rubber film or coated rubber parts, a freeze dryer might be better for very slow, controlled drying. But 99% of manufacturing use cases for rubber—molded parts, hoses, gaskets, seals—drying ovens are the most cost-effective, fastest option. Way cheaper than freeze drying, way more consistent than air-drying in a warehouse for 24 hours (which leads to dust and contamination too, by the way). Air-drying is just asking for parts to get dirty, or absorb more moisture if the warehouse is humid, so that’s a no-go for most production lines.
Let me throw in a real customer example to make this concrete. A auto parts client of mine makes rubber hoses for cooling systems. For years, they’d pressure-wash the molded hoses after demolding, then set them outside on pallets to air-dry for 12 hours. Problem was, half the time they’d get rejected because of moisture left in the hose walls—causing coolant leaks after installation. They bought our batch drying oven, set it to 160°F, with medium air flow, and now they dry every batch in 2 hours. Rejection rate for moisture issues dropped to almost zero, and they saved like 10 man-hours a day that they used to spend moving pallets around the yard. That’s the kind of win we’re talking about.
Another thing to keep in mind: if your rubber has any residual solvent from the manufacturing process (like if you used a solvent-based adhesive during bonding), a drying oven is perfect for that too, as long as you pick one that’s explosion-proof if the solvent is flammable. That’s a key feature for rubber processing—no one wants to deal with fumes building up and causing a hazard. Our ovens all have venting systems that pull fumes outside, so you don’t have to worry about that.
Wait, what about post-curing? A lot of people confuse drying rubber with post-curing, and that’s a big mix-up. Post-curing is when you heat cured rubber to finish the cross-linking process, which changes its physical properties (makes it more durable, heat-resistant). Drying is just removing moisture. So if you’re using a drying oven for drying, you don’t want to set it to post-cure temps—stick to the lower range. If you need to do both, you can adjust the settings after drying, but that’s a separate step.
Now, let’s wrap this up with the actual takeaway for anyone reading this: Yes, a drying oven can absolutely be used for drying rubber products, but only if you match the oven to your specific rubber type, use the right settings, and follow basic drying best practices. The days of ruining batches with hot ovens or weak air flow are over—you just need the right setup.
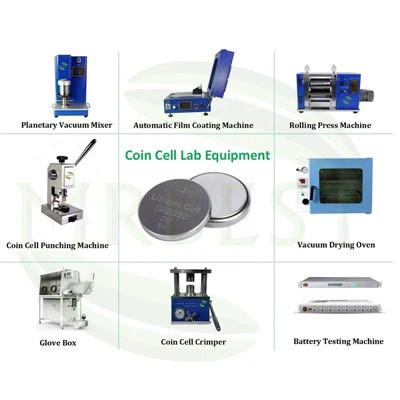
If you’re tired of dealing with moisture-related scrap, slow drying times, or inconsistent results in your rubber processing, I’m here to help. We work with rubber manufacturers of all sizes—from small shops making custom gaskets to large factories producing automotive hoses—to customize drying oven setups that fit their exact needs. Whether you need a small batch oven for R&D, a conveyor oven for high-volume production, or something in between, we can walk you through testing, settings, and everything you need to get your drying process right. Don’t waste another batch of rubber because of bad drying—reach out to our team to chat through your needs, and we’ll help you find the solution that works for you.
Pin Type Supercapacitor References:
- Handbook of Rubber Processing and Properties, 2nd Edition, Smith, A., Wiley, 2020.
- Industrial Drying Principles and Practice, Mujumdar, A.S., Taylor & Francis, 2015.
- ASTM D1566-21, Standard Terminology Relating to Rubber, ASTM International, 2021.
- "Moisture Control in Rubber Manufacturing Processes", Journal of Rubber Research, Vol. 22, No. 3, 2019, pp. 189-202.
- Industrial Convection Ovens: Selection and Application Guide, NIST Special Publication 1180, 2017.
Shenzhen Meirui Zhida Technology Co., Ltd.
Shenzhen Meirui Zhida Technology Co., Ltd. is one of the most professional drying oven manufacturers and suppliers in China, specialized in providing high quality products with low price. If you’re going to buy bulk discount drying oven made in China, welcome to get pricelist and quotation from our factory.
Address: 104 Building 6, Second Industrial Zone, Shanmen Community, Yanluo Street, Baoan District, Shenzhen China
E-mail: mrbest@szmrbest.com
WebSite: https://www.szmrbest.com/
